How to Choose a Conveyor System Manufacturer for Custom Material Handling
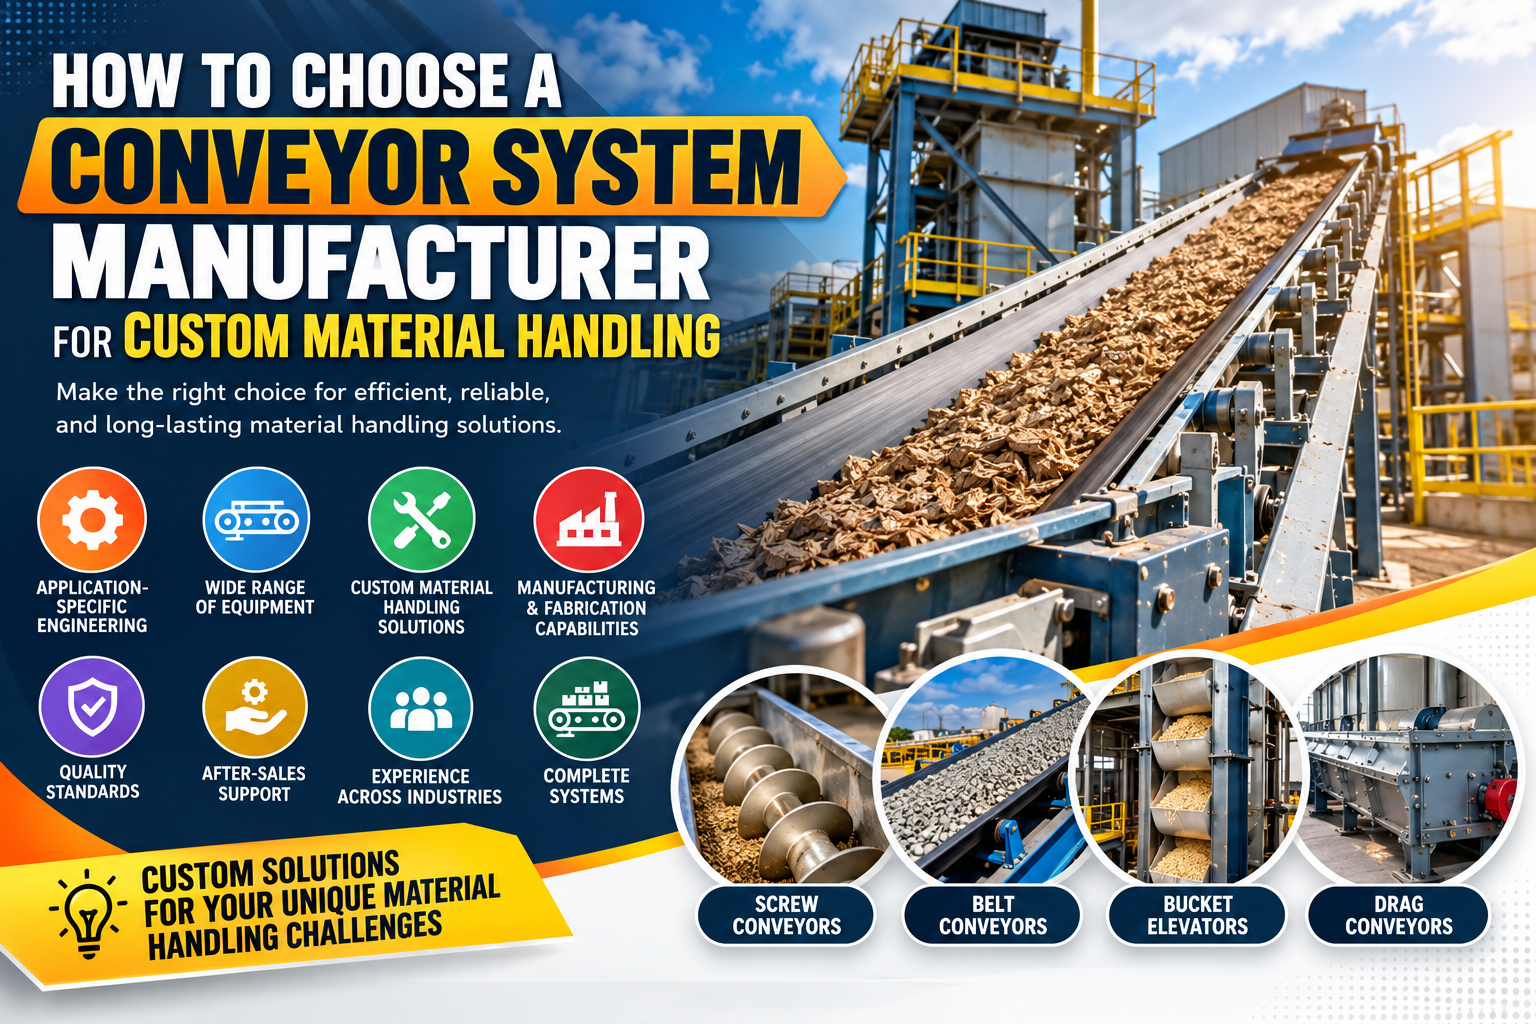
Selecting the appropriate Conveyor System Manufacturer is an essential step in the case of any organization which relies on its conveyor systems to transport bulk materials. Regardless of whether you are dealing with agricultural products, chemicals, food products, wood materials, wastewater, or any other industrial bulk solids, your conveyor system will have to suit your specific process.
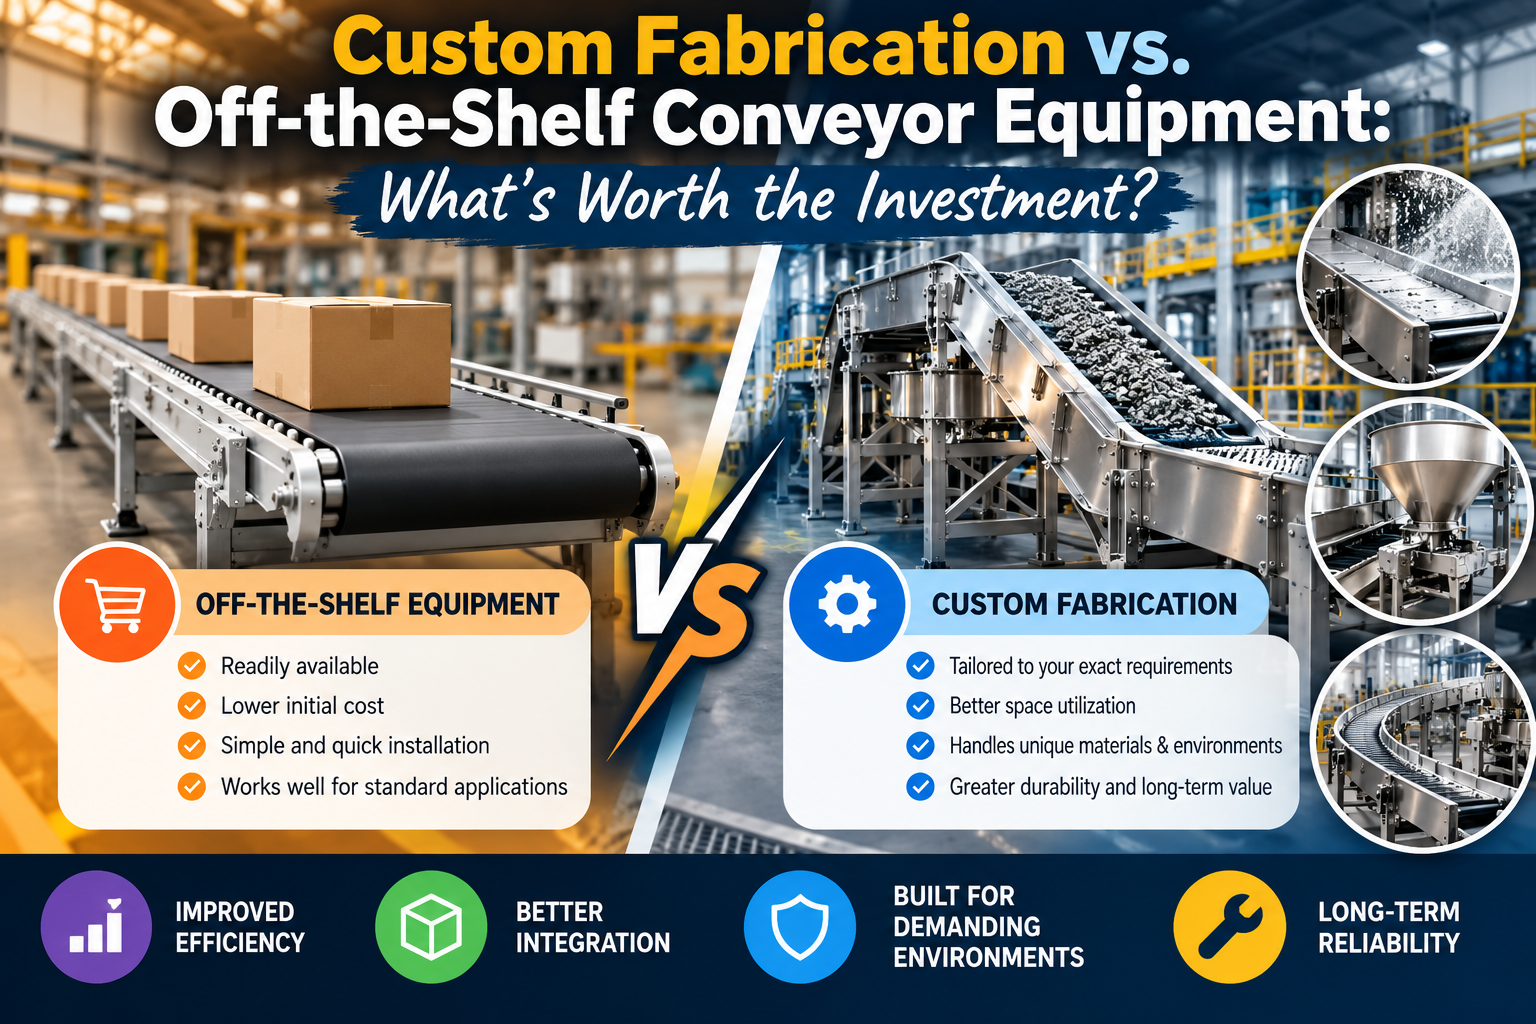
While off-the-rack solutions might work fine for simple applications, customized material handling systems are needed for complicated installations, taking into account all factors such as material properties, processing volume, plant structure, and environmental conditions. Your conveyor system manufacturer should do much more than provide a conveyor system.
1. Look for Application-Specific Engineering
All material handling situations present unique challenges. Density, particle size, moisture content, temperature, abrasion resistance, flow ability, and required throughput levels may impact how a particular conveyor performs.
A reputable Conveyor System Manufacturer would do well to consider all of these parameters rather than recommend equipment strictly on capacity or cost alone.
Conveyors Inc., for instance, specializes in custom engineered bulk material handling solutions in industrial applications. Its product line includes screw conveyors, belt conveyors, drag conveyors, bucket elevators, shaftless conveyors, vertical screw conveyors, feeders, and complete conveyor systems.
2. Evaluate the Manufacturer's Range of Equipment
A wide range of equipment offered by a particular manufacturer allows for more flexibility during the custom system development.
Various conveying techniques are effective at overcoming various problems related to materials transportation. Screw conveyors offer controlled feeding and material flow, and belt conveyors are used for long-distance continuous transporting. Drag conveyors are effective at enclosed and heavy-duty material transport, and bucket elevators allow moving bulk materials vertically.
In some cases, special techniques such as shaftless conveyors and customized fabricated parts can be required for the efficient conveying. All the above mentioned technologies are provided by Conveyors Inc. within its range of industrial conveyors.
During the choice of a manufacturing company, make sure the company is capable of evaluating different technologies rather than applying a universal conveying system design.
3. Ask About Custom Material Handling Systems
Facility design itself can complicate the installation of conventional equipment.
The presence of other machinery, space constraints, elevation differences, conveyance points, discharge points, and the process itself might necessitate some adjustments.
This is where Custom Material Handling Systems come into play.
A producer needs to be able to design equipment according to the layout of the facility instead of redesigning the facility to accommodate the equipment.
Conveyors Inc. produces fully integrated material handling systems, which include several types of conveying equipment along with hoppers, bins, chutes, transitions, and automated slide gates.
A one-stop approach will also assist in proper equipment alignment and installation since all parts of the system will be designed to work together.
4. Consider Manufacturing and Fabrication Capabilities
Only the engineering aspect of the conveyor system is not enough for making the conveyor system work efficiently. There is another factor that is equal to the first one.
The capability of the company to make the components according to the required specifications is also important.
The conveyor company called Conveyors Inc. is able to make custom fabricated components in response to specific wear, layout, and capacity issues. The company also offers services for making custom components, mixers, blenders, classifiers, and other application-specific equipment.
While selecting the right manufacturer, consider whether the company has the capability to make custom components.
5. Check Standards and Quality Practices
It is vital that the industrial machinery be constructed to cope with its operating environment. This may involve coping with an abrasive environment, corrosive goods, high temperature, dust, moisture, or extensive operating cycles.
It is essential that any good manufacturer has certain engineering and manufacturing standards.
Conveyors Inc. supplies standard CEMA industrial conveyors, as well as special-purpose machinery intended for tough duty operation. The range of machinery produced by the company meets the needs of tough bulk material handling applications.
In particular cases, manufacturers need to be able to recommend proper materials, components, liners, seals, and construction techniques.
6. Look Beyond the Initial Purchase
The price of a conveyor is just one element of its value.
Maintenance, spare parts, breakdowns, energy use, setup, and equipment longevity may all have an impact on the ultimate cost of ownership.
As a result, it is critical to select a manufacturer who can offer support following installation.
Conveyors Inc. offers replacement parts in accordance with CEMA standards and custom parts to enable upgrades, retrofits, and general equipment maintenance.
Additionally, manufacturers who comprehend the original design will be in a better position to assist with alterations or replacement parts later in the lifetime of the equipment.
7. Review Experience Across Different Industries
Another aspect that might influence selection of a Conveyor System Manufacturer is industry experience. Manufacturers working in various industries will likely have experience of tackling more complex material handling issues.
Conveyors Inc. offers bulk material handling systems for a variety of industries, such as agriculture, alternative fuels, chemicals, wastewater, food products, and lumber and wood products. Different industries require different material properties to be handled in various environmental conditions.
Thus, industry experience might prove extremely valuable when dealing with unusual materials and harsh conditions.
8. Choose a Manufacturer That Can Handle Complete Systems
Some projects may involve the use of considerably more than one conveyor on their own.
In such instances, coordinating with manufacturers who have the ability to provide an entire system may be easier to coordinate for your project.
At Conveyors Inc., we supply complete bulk material handling systems, which include conveyors and other components such as hoppers, bins, chutes, transitions, and automatic gates.
This is one way of ensuring that your components will fit together seamlessly in the material flow process.
Make the Right Choice for Your Material Handling Application
Choosing a Conveyor Systems Manufacturer should never be solely dependent on the equipment cost or a standard list of available products. The best choice will be made when you find a company that knows about your material, throughput, plant layout, operating conditions, maintenance needs, and future plans.
For those facilities which require special material handling systems, Custom Material Handling Systems are much better than trying to fit an existing process in the standard conveyor configuration. The best manufacturer can use various technologies to design the required Industrial Conveyor Systems.
The variety of technologies, custom fabrication, and systems integration solutions allow Conveyors Inc. to offer equipment for tough bulk material handling applications.
When your facility requires a custom conveyor or material handling system, talk first about your material, capacity, layout, and operating conditions with the experienced manufacturer. With the properly designed system, you will achieve effective material transport and productivity.
Are you ready to talk about your project? Conveyors Inc. offers custom quotes for material handling systems for specific applications.